Pump Applications
A Practical Guide to Pump Selection Across the Mining Process
Published on
14 October 2026
Choosing Mining Pumps: Where AODD and Peristaltic Perform Best, Stage by Stage
Why Positive Displacement Pumps Suit Mining Applications
Positive displacement pumps are well suited to mining applications because they deliver consistent, controllable flow even when slurry density, solids content, or backpressure fluctuate. While centrifugal slurry pumps remain common across many high-volume transfer duties, Air-Operated Double Diaphragm (AODD) and Peristaltic pumps offer distinct advantages where conditions are variable, abrasive, or chemically aggressive. The ability of these pumps to run dry, self-prime, handle abrasive solids, and operate reliably under varying pressures makes them a practical choice at many of the more demanding points in the mining circuit.
Mining is one of the most demanding environments for pumping equipment. Slurries shift in density, solids content changes hour by hour, and chemical conditions vary from neutral to highly corrosive. The choice between an AODD pump and a Peristaltic pump can make the difference between smooth operation and constant maintenance.
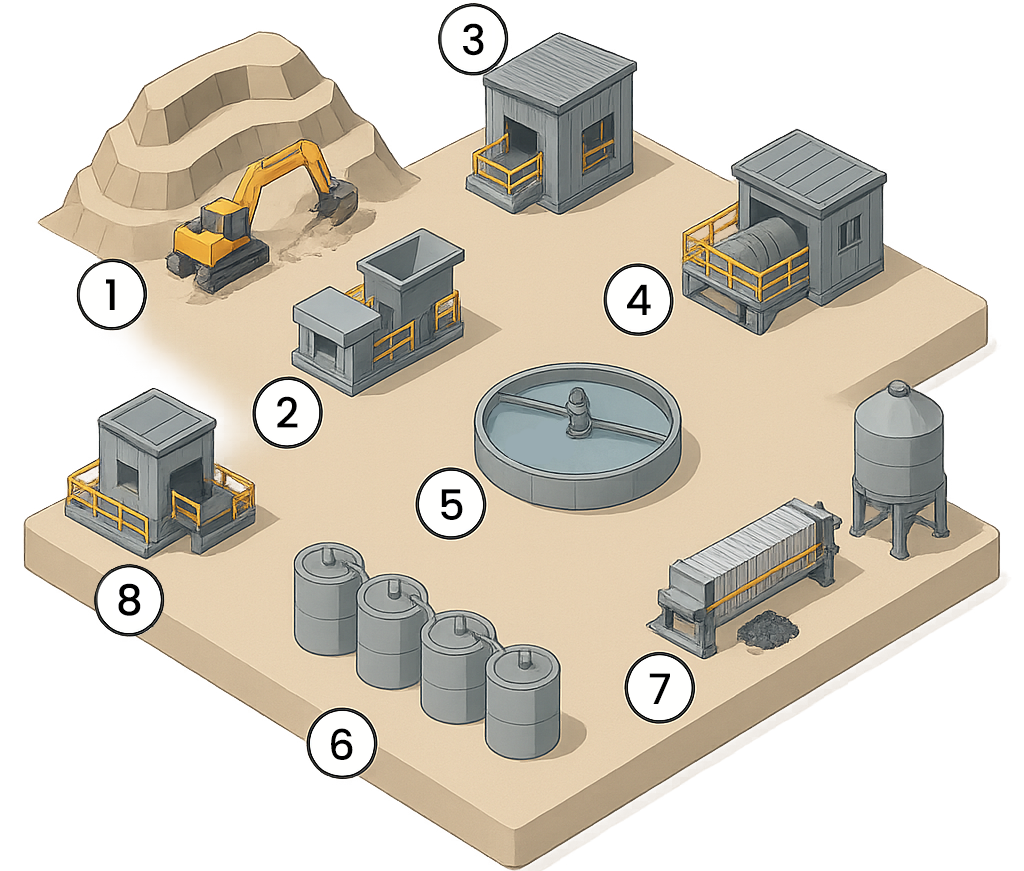
To help simplify pump selection across the full mining circuit, we have created the illustrated process diagram above. This visual highlights every stage, excavation, crushing, screening, milling, thickening, leaching, dewatering, and load-out, where pumps play a critical role.
1. Open-Pit Mining (Dewatering Pumps)
Media: Dirty water, runoff, mud, overburden wash
Challenges: Abrasion, solids, unpredictable conditions, temporary pump locations
Pump Role: Dewatering, sump cleaning, emergency removal
Best Pump: AODD AODD
For large-scale pit dewatering, particularly where high flow volumes are required continuously, submersible and centrifugal pumps are more commonly deployed. AODD pumps are the practical choice for sump cleaning, emergency removal, and temporary or repositionable duties where compressed air is available and electrical supply is not. Their ability to run dry, handle solids-laden runoff, and self-prime without setup time makes them well suited to the unpredictable, shifting nature of active excavation areas.
2. Primary Crusher (Coarse Size Reduction)
Media: Coarse slurry, rock fines, wash-down water
Challenges: Harsh abrasion, debris-filled sumps, inconsistent flow
Pump Role: Clearing crusher sumps and removing runoff
Best Pump: AODD AODD
At high-throughput operations, centrifugal slurry pumps are frequently used for crusher sump duty given their capacity for continuous, high-volume transfer. AODD pumps are preferred where sumps are smaller, access is restricted, flow is intermittent, or where the installation cannot justify a fixed centrifugal setup. Their ball-and-seat check valve design tolerates coarse debris and inconsistent flow without cavitation, and they can be repositioned or replaced without significant downtime.
3. Screening Station (Sizing and Separation)
Media: Spray water, fines, variable-density slurry
Challenges: Continuous abrasion, variable slurry density, surging flow
Pump Role: Sump transfer and fines slurry movement
Best Pump: AODD or Peristaltic AODD Peristaltic
AODD pumps suit light to medium density slurry (SG below roughly 1.3) where flow is intermittent or the pump may need to be repositioned. If the fines slurry is consistently high density, runs continuously, or requires pulseless flow to protect downstream equipment, a Peristaltic pump is the more appropriate selection.
4. Grinding Mill (SAG/Ball Mill Discharge)
Media: Thick, highly abrasive slurry
Challenges: Severe abrasion, high viscosity, continuous operation
Pump Role: Transferring ground ore to classification
Best Pump: Peristaltic Peristaltic
Centrifugal slurry pumps, used widely in SAG and ball mill circuits at large-scale operations, remain the most common technology for mill discharge transfer due to their high flow capacity. Where Peristaltic pumps are selected at this stage, the rationale is typically maintenance-driven: only the hose contacts the slurry, eliminating internal wear on impellers, casings, and seals. This makes them attractive where abrasive ore is causing unacceptable wear rates on centrifugal pump components, where smaller mill throughputs do not justify the infrastructure of a centrifugal installation, or where consistent metered flow is required through to classification.
5. Thickener (Solids-Liquid Separation)
Media: Thick, paste-like underflow; clarified overflow
Challenges: Rising discharge pressure, extreme viscosity, density swings
Pump Role: Underflow transfer to filtration or additional thickening
Best Pump: Peristaltic Peristaltic
Thickener underflow is one of the more established applications for Peristaltic pumps in mining operations, where paste-like underflow densities and rising discharge pressure can cause centrifugal alternatives to choke or lose prime. Progressive cavity pumps are also used at this stage and can handle similar viscosities, but require more careful management of solids content to avoid stator wear. The selection rationale for Peristaltic here is typically a combination of pressure tolerance, the ability to handle density swings without intervention, and lower sensitivity to grit and abrasives in the media.
6. Leaching / Conditioning Tanks (Chemical Treatment)
Media: Slurry mixed with acids, alkalis, and reagents
Challenges: Corrosion, abrasion, dosing accuracy, chemical compatibility
Pump Role: Slurry movement, reagent addition, pH adjustment
Best Pump: Peristaltic (slurry) + AODD (chemicals) Peristaltic AODD
For leach slurry transfer, Peristaltic pumps are selected where chemical corrosion and abrasion together would rapidly degrade the wetted components of alternative pump types, as the hose-only contact eliminates this combined attack. Progressive cavity pumps are also used in leach slurry service and can be appropriate where flow rates exceed Peristaltic capacity, though stator compatibility with the specific reagent chemistry must be verified. For reagent dosing specifically, acids, alkalis, and oxidants, AODD pumps constructed in PVDF or PTFE are a common and well-suited choice due to their chemical resistance, controllable flow at low volumes, and the ability to shut off safely without backflow.
7. Filter Press (Dewatering)
Media: High-density slurry, filtrate, filter cake
Challenges: Pressure spikes, heavy solids loading
Pump Role: Filter press feed and filtrate return
Best Pump: Peristaltic (feed) + AODD (filtrate) Peristaltic AODD
Filter press feed is one of the well-documented Peristaltic pump applications in mineral processing. As the filter press fills and internal pressure rises toward final squeeze pressure, a Peristaltic pump continues to deliver against the rising pressure, maintaining feed rate without operator intervention or bypass valving. This pressure-adaptive behaviour is the primary selection rationale over centrifugal pumps, which lose flow as backpressure rises. For filtrate return, AODD pumps are appropriate: filtrate is relatively clean, flow is intermittent as chambers drain, and the self-priming capability avoids the need for additional priming equipment.
8. Final Concentrate Storage (Load-Out)
Media: Dense mineral concentrate slurry, semi-dry solids
Challenges: High SG, variable viscosity
Pump Role: Transfer, recirculation, loading
Best Pump: Peristaltic or AODD Peristaltic AODD
At this stage, pump selection is typically driven by concentrate density and duty type. Progressive cavity pumps are also widely used for dense concentrate transfer given their tolerance of high SG slurries and smooth, pulseless output. Peristaltic pumps are preferred where abrasion or chemical content would cause unacceptable stator wear in a progressive cavity pump, or where hose replacement offers a lower total maintenance cost than stator and rotor replacement cycles. AODD pumps suit mobile loading operations, intermittent transfer duties, or installations where compressed air infrastructure is already available and electrical connection is impractical.
Summary Table – Best Mining Pumps by Stage
| Stage | Media | Challenge | Best Pump |
|---|---|---|---|
| 1 | Dirty water, sludge | Portability | AODD |
| 2 | Crusher sump slurry | Abrasion | AODD |
| 3 | Screen deck slurry | Variable solids | AODD / Peristaltic |
| 4 | Mill discharge slurry | Abrasion and viscosity | Peristaltic |
| 5 | Thickener underflow | Paste-like viscosity | Peristaltic |
| 6 | Leach slurry, reagents | Chemical and abrasive | Peristaltic (slurry) / AODD (reagents) |
| 7 | Filter press feed, filtrate | Rising pressure | Peristaltic (feed) / AODD (filtrate) |
| 8 | Concentrate slurry | High SG | Peristaltic / AODD |
Need help selecting the right pumps for your mining application? Our specialists are here to help.
Contact Enviroflex